


At LINKOOL, commercial refrigeration quality is not measured only by the appearance of a finished refrigerator.
It starts with the materials entering the factory, continues through every production process, and ends with inspection, testing and customer feedback.
To make this process more transparent for our global B2B customers, LINKOOL is introducing regular quality updates covering incoming inspection, first-pass yield, major quality incidents, customer feedback and continuous improvement projects.
This month's data shows stable overall quality performance, while one specific production improvement has reduced the defect rate of an internal lighting connection from 4% to 0%.
Our quality team continuously monitors key indicators across incoming materials, production and customer feedback.
| Quality Indicator | Current Performance | Change / Status |
|---|---|---|
| Incoming Material Inspection Pass Rate | 98.3% | +0.02% |
| First-Pass Inspection Pass Rate | 98.1% | +0.5% |
| Major Quality Incidents | 0 | No major incident |
| Customer Quality Feedback | 3 cases | Mainly external glass damage |
| Continuous Improvement Projects | 8 total | 1 ongoing, 7 completed |
These figures are part of LINKOOL's internal quality monitoring process and are used to identify potential problems before they become larger production or customer issues.
Rather than reporting only successful results, we believe transparent quality reporting should also explain what went wrong, why it happened, what was changed and whether the change worked.
The incoming material inspection pass rate reached:
This represents a 0.02 percentage-point improvement compared with the previous reporting period.
Incoming inspection is an important first control point in commercial refrigeration manufacturing.
Before materials enter production, quality inspection can be used to identify potential issues involving:
The objective is straightforward:
Do not allow a material problem to become a production problem.
For a commercial refrigerator manufacturer, controlling quality at the incoming stage helps reduce the risk of defects being transferred into subsequent manufacturing processes.
LINKOOL's first-pass inspection rate reached:
This represents a 0.5 percentage-point improvement compared with the previous reporting period.
First-pass yield is an important production-quality indicator because it reflects how many products or processes meet the defined inspection requirements without requiring rework or repeated inspection.
A higher first-pass inspection rate generally means fewer resources are consumed by:
However, LINKOOL does not treat the first-pass rate as the only quality indicator.
A high first-pass rate must be considered together with incoming material quality, process inspection, final inspection, customer feedback and continuous improvement.
During this reporting period, LINKOOL recorded:
0 major quality incidents.
This means there was no major quality event requiring classification as a significant production or product-quality incident during the reporting period.
However, zero major incidents does not mean that no problems occurred.
In manufacturing, smaller abnormalities are often valuable sources of information.
This is why LINKOOL also tracks:
The goal is not simply to react to major problems.
The goal is to identify smaller problems early and eliminate their root causes before they develop into larger issues.
During the reporting period, LINKOOL recorded:
The main reported issue was:
Glass breakage caused by external factors.
Glass is an important component in commercial display refrigerators and freezers because it provides product visibility while separating the refrigerated cabinet from the surrounding environment.
However, glass can also be affected by:
For this reason, customer feedback needs to be investigated according to the actual failure condition rather than automatically classifying every glass breakage as a manufacturing defect.
For each relevant case, the quality team can evaluate factors such as:
Product condition → Packaging → Transportation → Handling → Installation → External impact
This type of traceability helps distinguish between manufacturing-related issues and external damage.
It also provides valuable information for improving packaging, transportation protection and customer handling instructions where necessary.
One of the most meaningful quality-improvement cases this period involved an internal cabinet light that failed to illuminate.
At first glance, a light not turning on may appear to be a minor electrical problem.
However, for a commercial display refrigerator, internal lighting directly affects product visibility.
A failed light can result in:
Therefore, LINKOOL's quality team investigated the problem instead of simply replacing the light.
The investigation identified the root cause as:
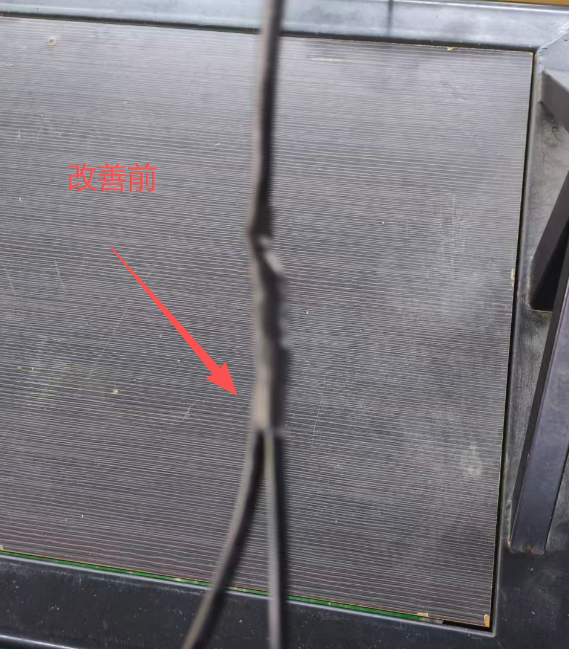
The original connection process used:
Piercing + Copper Clip + Heat-Shrink Tubing
Although this connection method could complete the electrical connection, the quality team identified the connection point as a potential source of instability.
This led to the next step:
Instead of repeatedly repairing the same failure, can the connection process itself be improved?
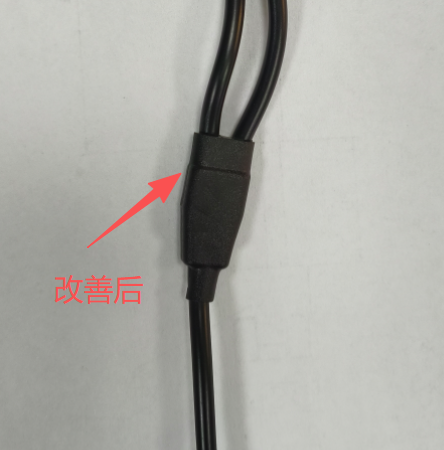
LINKOOL changed the connection method.
Piercing → Copper Clip → Heat Shrink
Welding → Injection Molding
The new process provides a more controlled connection structure and reduces the risk associated with poor contact at the original connection point.
The improvement was not simply a component replacement.
It was a process-level improvement.
This distinction is important.
A temporary repair solves an individual failure.
A process improvement aims to prevent the same failure from occurring repeatedly.
The most important part of a quality improvement project is not the description of the change.
It is the measurable result.
Before the process improvement:
After implementing the new connection process:
| Item | Before Improvement | After Improvement |
|---|---|---|
| Light Connection Method | Piercing + Copper Clip + Heat Shrink | Welding + Injection Molding |
| Main Failure | Poor Electrical Contact | No observed defect in the reported improvement result |
| Defect Rate | 4% | 0% |
The result indicates that the improved connection process significantly reduced the identified lighting-connection defect in the relevant production evaluation.
For technical accuracy, the 0% figure should be understood within the tested production sample and reporting period, rather than interpreted as a guarantee that this component can never fail.
That distinction is important for transparent quality reporting.
For a supermarket or convenience store, an internal LED light may seem like a small component.
But commercial refrigeration is a system made up of many individual components.
A small component failure can create a much larger operational impact.
For example:
Light Connection Failure
↓
LED Does Not Illuminate
↓
Reduced Product Visibility
↓
Poorer Display Performance
↓
Potential Service Requirement
↓
Additional Maintenance Cost
This is why component-level quality improvements matter.
A reliable commercial refrigerator is not created by one major component alone.
It is the result of controlling hundreds of individual manufacturing details.
LINKOOL's approach can be summarized as:
Detect an abnormality through production inspection or customer feedback.
Determine where and when the problem occurs.
Separate the actual cause from the visible symptom.
Modify the process, component or manufacturing method.
Measure the result after the improvement.
If the improvement is effective, incorporate the new process into the relevant production standard.
This creates a continuous improvement loop:
Detection → Analysis → Improvement → Verification → Standardization
LINKOOL currently has:
including:
This reflects an important principle in manufacturing:
Quality is not a one-time inspection. It is a continuous process.
A product may pass final inspection today, but manufacturing teams should still look for opportunities to improve:
Continuous improvement allows manufacturers to gradually reduce process risk rather than waiting for customer complaints to reveal every problem.
For an importer, distributor or supermarket group, choosing a commercial refrigeration manufacturer involves more than comparing product prices.
Buyers also need to evaluate:
Can the manufacturer maintain stable quality across repeated production?
Are problems identified during manufacturing rather than after shipment?
Can the factory identify root causes instead of simply replacing defective components?
Will the manufacturer communicate quality problems honestly?
Does the manufacturer improve processes based on actual production data?
These factors directly influence the long-term cost and reliability of commercial refrigeration procurement.
LINKOOL believes that quality communication should not only happen when customers ask about a problem.
It should become part of normal communication with B2B customers.
That is why we plan to continue monitoring and publishing key quality indicators such as:
The purpose is not to claim that manufacturing is perfect.
The purpose is to show how quality is measured, how problems are handled and how production processes improve over time.
For customers sourcing commercial refrigeration equipment, these quality-management practices provide an additional layer of visibility into the manufacturing process.
LINKOOL's approach focuses on:
Measure → Identify → Improve → Verify → Standardize
From incoming materials to production processes and customer feedback, each stage provides information that can be used to improve the next production cycle.
The lighting-connection improvement is one example.
The reduction from 4% to 0% demonstrates how a relatively small production-process change can produce a measurable improvement in a specific quality indicator.
LINKOOL manufactures commercial refrigeration equipment for global B2B markets, including:
Our quality-management approach is based on more than final product inspection.
It includes:
Incoming Material Control
↓
Production Process Inspection
↓
Final Product Inspection
↓
Performance Testing
↓
Customer Feedback
↓
Root-Cause Analysis
↓
Continuous Improvement
For global distributors, importers, supermarket groups and commercial refrigeration buyers, this provides a more transparent view of how LINKOOL manages product quality.
Incoming Material Inspection Pass Rate
First-Pass Inspection Rate
Major Quality Incidents
Customer Quality Feedback Cases
Continuous Improvement Projects
Lighting Connection Defect Rate After Process Improvement
A manufacturer can say:
“We provide high-quality refrigeration equipment.”
But a more meaningful question is:
How is quality measured?
At LINKOOL, we believe the answer should be supported by data, manufacturing processes, inspection records and continuous improvement.
We will continue to monitor our quality indicators and share representative improvement cases with our B2B customers.
Because reliable commercial refrigeration is not created by inspection alone.
It is built through continuous control, measurement and improvement.
LINKOOL — Commercial Refrigeration Manufacturer for Global B2B Markets.
 Sweden Supermarket Refrigeration Case Study | Custom Glass Door Display Refrigerators
 Beverage Refrigeration Solutions for Different Climates, Store Formats & Retail Needs
 LINKOOL Modular Commercial Freezer System | One Compressor Dual Cabinet Refrigeration Technology
 LINKOOL Team Building Event: Strengthening Our Family Culture Beyond Commercial Refrigeration Solutions
